A small turned part looks simple on the drawing, and that is exactly why it is easy to quote on the wrong process. A pin 2 mm in diameter and 30 mm long, a miniature shaft with three diameters and a thread, a bushing with a cross-hole and a groove — these are the parts where conventional turning starts to struggle, not because the machine cannot cut them, but because the part itself will not stay still while it is cut. Swiss turning exists for this problem. It supports the workpiece almost at the point of cut, and that one difference changes what is possible for small, slender, and detail-rich parts.

What Swiss turning actually does differently
In conventional turning, the bar is held in a chuck or collet and the tool works some distance away from the support. The longer and thinner the part, the more it flexes under cutting force, and the more it vibrates. The result is taper, chatter marks, poor surface finish, and dimensions that drift from one part to the next.
A Swiss-type lathe — also called a sliding-headstock lathe — feeds the bar through a guide bushing, and the cutting happens just past the bushing. The support is always close to the cut, no matter how long the part is. The bar slides forward as work progresses, and the tools wait at the bushing. Because the unsupported length is always short, a slender part stays rigid while it is machined. That is the whole principle, and it is why Swiss turning is the standard process for long, thin parts.
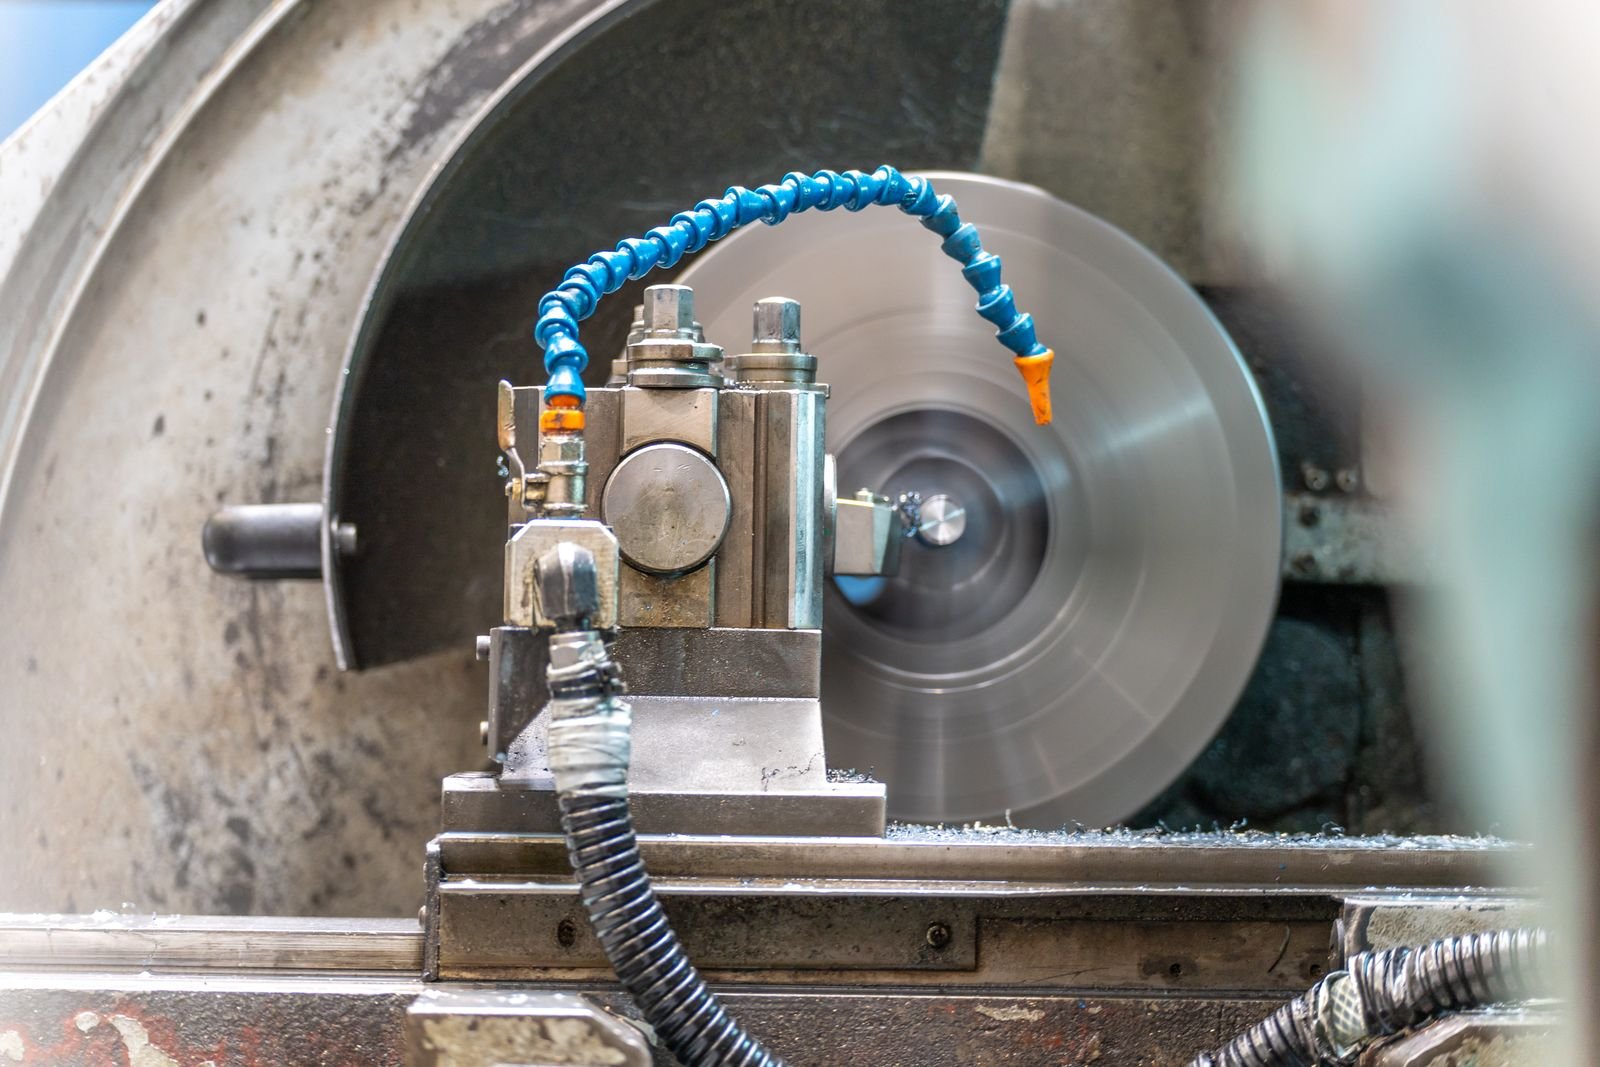
There is a second difference that matters just as much. A Swiss lathe typically carries many tools — main-spindle tools, sub-spindle tools, and live tools for milling and drilling — and can complete turning, milling, cross-drilling, and threading in one setup. A part that would need three setups on a conventional lathe, with re-clamping and re-alignment each time, can come off a Swiss machine finished. Fewer setups means fewer chances for alignment to shift, and for small parts that is often the difference between a batch that measures consistently and one that does not.
The parts that point to Swiss turning
Precimora’s Swiss turning capability lists pins, bushings, miniature shafts, and multi-feature turned parts as typical components, and that list is a good test for your own part. Ask whether your part looks like one of these.
A long, slender pin or shaft is the clearest case. As a rule of thumb, when the length of a part is more than about three to four times its diameter, conventional turning without extra support becomes difficult, and the difficulty grows fast with length. A shaft 3 mm in diameter and 25 mm long is eight times its diameter — a Swiss machine handles that routinely, because the guide bushing supports the work at the cut. If your drawing has a long, thin section, say so in the RFQ, and ask whether Swiss turning is the intended process.
A miniature part with several features is the second case. A small connector body with a thread, a groove, a cross-hole, and a flat is not hard because any single feature is hard — it is hard because each feature needs its own setup on a conventional machine, and each setup on a part a few millimetres across is a chance to lose alignment. On a Swiss machine the features are cut in one cycle, so their positions relative to each other stay consistent.
A part that needs tight repeatability across a batch is the third case. Because the bar feeds through the bushing and the tools do not move relative to the support, Swiss turning holds dimensions consistently from the first part to the thousandth. If your assembly depends on every part in the batch measuring the same, rather than on a single part measuring right, that consistency is worth asking about.

What Swiss turning does not fix
Swiss turning is not a cure for every small part. It does not fix a bad drawing, a wrong material, or a tolerance that is tighter than the function needs. And it has its own limits. The guide bushing needs bar stock that is straight and consistent in diameter, because the bar slides through the bushing — bar that varies in size will bind or wobble. Very large diameters are outside the Swiss range; the process is for small parts, and a part that is large in diameter belongs on a conventional lathe. Deep internal features can still be difficult, because the tool must reach inside the part regardless of how the outside is supported.
The practical point is to let the supplier choose the process. Precimora reviews material, tolerances, surface finish, inspection, and quantity against the drawing before quoting, and the process route — conventional turning, Swiss turning, or a combination — is part of that review. A buyer who states the part’s length-to-diameter ratio, its features, and its batch consistency requirement, and then asks which process the quote assumes, will get a better answer than a buyer who demands Swiss turning by name for a part that does not need it.
How to state a Swiss-turned part in your RFQ
The RFQ for a Swiss-turned part needs the same foundations as any turned-part RFQ, plus three details that matter specifically here. First, the length-to-diameter ratio and the longest slender section, so the supplier can see the deflection risk. Second, the full feature list — threads, cross-holes, flats, grooves — so the supplier can confirm the part can be completed in one setup or say which features need a second operation. Third, the batch consistency requirement: whether the assembly needs every part to measure the same, and which dimensions are the ones that must repeat.
Also state the material and the bar-stock condition if you know it. Free-cutting brass such as CW614N or C36000 machines well on Swiss lathes, which is one reason brass is a common Swiss-turned material, but the choice still depends on the part’s function. If the material is specified on the drawing, the supplier will review it; if it is open, say what the part must do and let the review recommend.
Common pitfalls and how to avoid them
The most common pitfall is quoting a slender part on a conventional process and then being surprised by taper, chatter, or inconsistent dimensions. The fix is to flag the length-to-diameter ratio in the RFQ and ask about the process route before the quote.
The second is assuming that Swiss turning automatically means tighter tolerances. It means better consistency on small, slender parts, but the tolerance still has to be stated on the drawing, and it still has to be achievable. A tolerance of ±0.02 mm on a critical diameter is achievable on request for Precimora’s turned parts, but it is a requirement to state, not a property of the machine.
The third is forgetting the bar-stock condition. If the drawing specifies a material but not the bar condition, the supplier will confirm it during review — but a buyer who knows the bar is centreless-ground or precision-drawn should say so, because it affects what the guide bushing can hold.
The fourth is designing a feature the Swiss process cannot reach. A deep internal bore, an undercut far from the end, or a feature on the back face that the sub-spindle cannot reach may still need a secondary operation. Ask during the engineering review which features are completed in the Swiss cycle and which need a second step, so the quote reflects the real route.
Buyer checklist
- The length-to-diameter ratio of the longest slender section is stated, and the deflection risk is visible on the drawing.
- Every feature — thread, groove, cross-hole, flat — is listed, so the supplier can confirm single-setup completion.
- The batch consistency requirement is stated: which dimensions must repeat across the batch, not just measure right once.
- The material is specified or the function is described so the supplier can recommend one.
- The tolerance is stated only where the function demands it; general dimensions rely on the general tolerance note.
- The process route (Swiss, conventional, or combined) is confirmed in the quote, not assumed.
- Any feature that may need a secondary operation is identified during the engineering review.
- The inspection plan covers the dimensions that must repeat, with first-article and in-process checks agreed.
If your part is small, slender, or rich in features, send the drawing for an engineering review and ask whether Swiss turning is the right route — state the length-to-diameter ratio, the feature list, and the batch consistency you need in the RFQ at https://precimora.com/request-a-quote/ — the quote is promised in 24–48h.